 Crypto.
 About
 Passport
 Conference call
 send money
 Terms
 Privacy
 Sierra market
Top Humidity Test Chamber Manufacturers for Pharmaceutical Testing
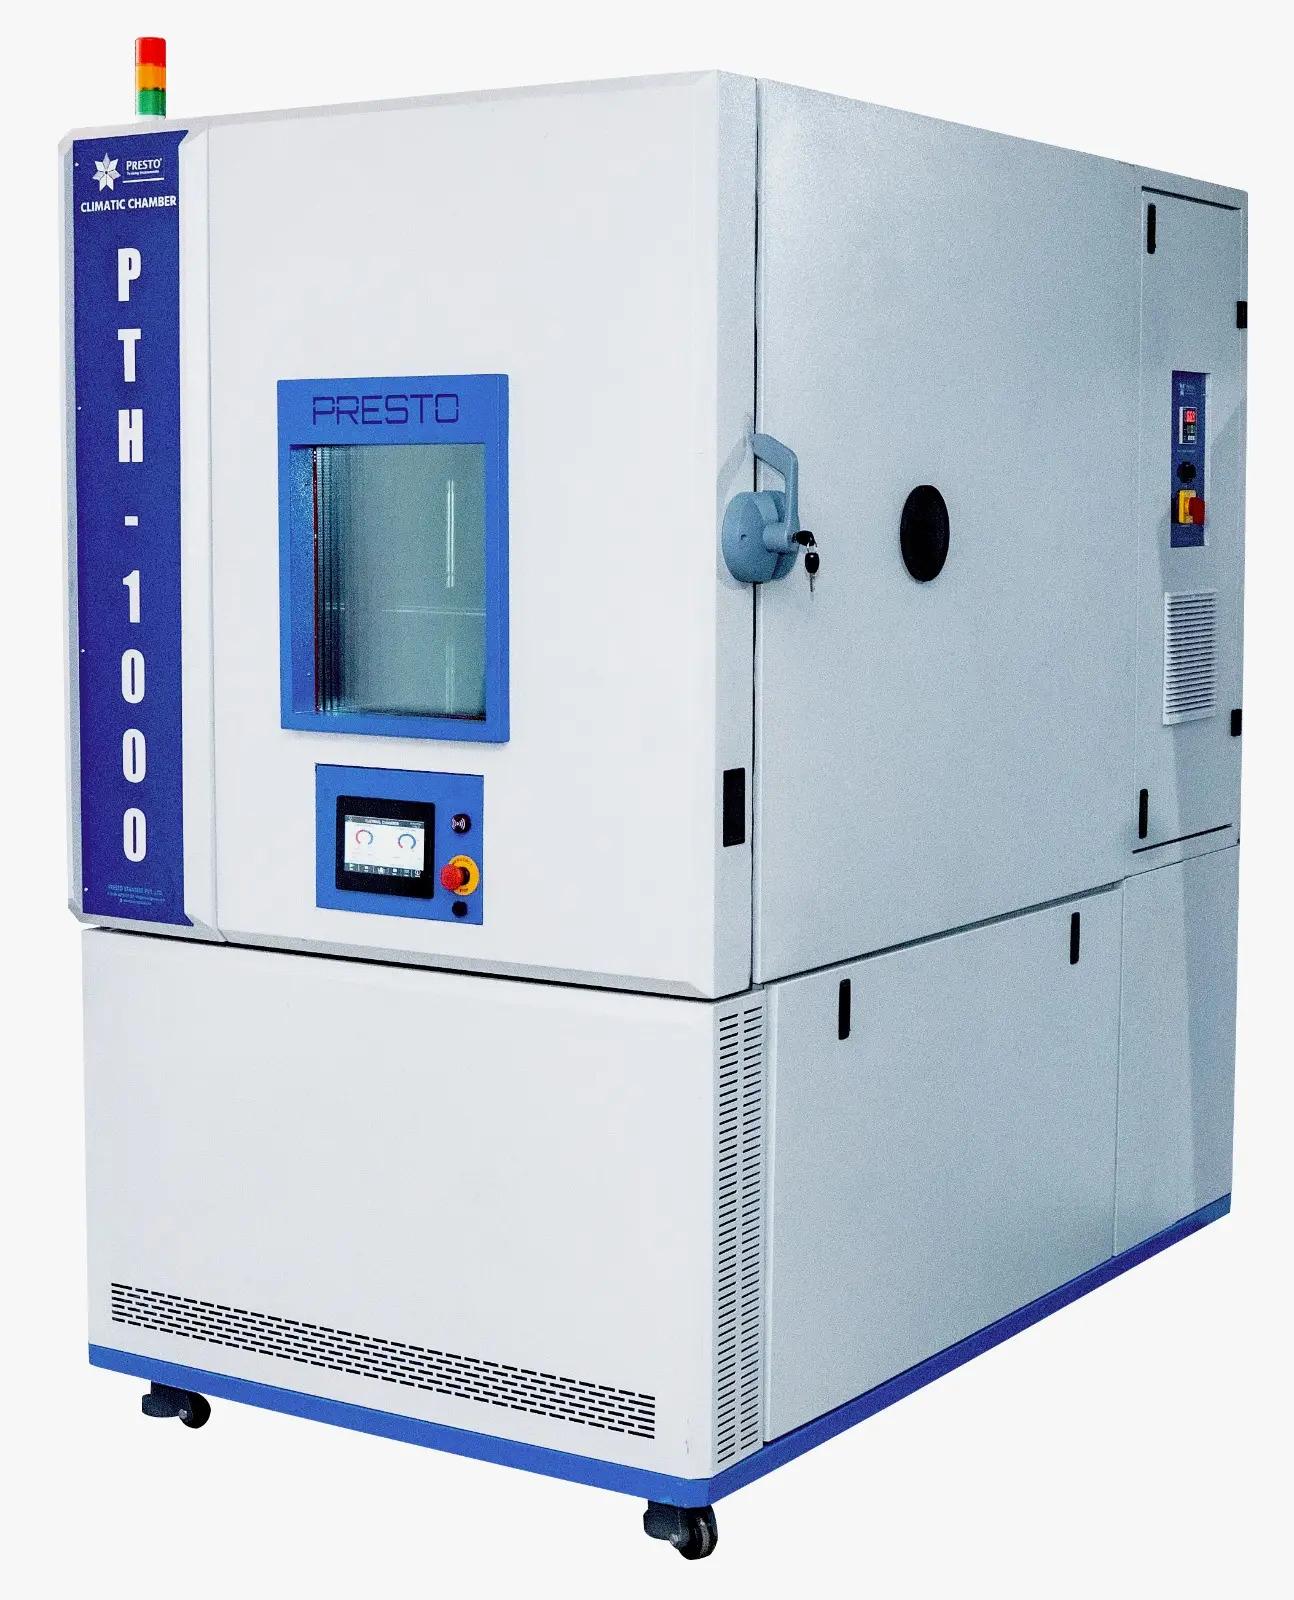
Pharmaceutical products require stability during storage and transport. Temperature variations alter drug chemical compositions and shorten shelf life. Every medicine needs proper climate checks before commercial release. A reliable humidity chamber creates accurate moisture conditions for exact stability analysis. Controlled environment simulation reveals potential package leaks or compound degradation. Modern drug developers depend on high precision equipment to satisfy strict regulatory standards. Safe medicine relies on thorough stress evaluation in controlled spaces. Accurate environmental simulation reduces commercial risk.
Top Humidity Test Chamber Manufacturers
Drug stability programs require high quality stress test gear from proven suppliers. The right equipment partner ensures uniform moisture output and reliable data for health authority approval.
Presto Enviro
Presto Enviro stands out as a leading humidity test chamber manufacturer in India. The company delivers top quality instruments designed for rigorous stability protocols. Labs rely on a humidity test chamber to simulate shelf life conditions for tablets, liquids, and capsules. Accurate sensors track minute shifts in moisture levels during extended evaluation runs. Internal chambers feature corrosion resistant stainless steel for long service life. Digital controls make parameter setup straightforward for lab technicians.
Laboratories with a humidity chamber from this supplier enjoy complete control over ambient factors. Microprocessor controllers maintain steady thermal settings across all sample shelves. Rapid recovery systems minimize climate drops during door openings. Built in safety alarms warn staff if moisture exceeds pre set boundaries. Sturdy locks keep chamber seals tight during extended humidity tests. Calibration options align with international standards for global market compliance.
Thermotron Industries
Thermotron Industries operates as a manufacturer of humidity test chambers for large industries worldwide. Facilities across the world use these systems for demanding environmental stress tests. Engineers design every humidity chamber with durable materials for continuous use. System software logs sample data automatically for audit trail records. Flexible interior configurations accommodate various package sizes and batch numbers.
Custom airflow designs protect sensitive pharmaceutical samples from hot spots. Multiple sensor probes verify chamber conditions across all interior corners. Energy efficient compressors keep operational costs manageable for large scale testing facilities. Remote monitoring tools allow operators to check test progress from distant workstations. Clear digital displays allow quick status updates for operators.
Weiss Technik
Weiss Technik is another well-known manufacturer of humidity test chambers recognized for precision. European pharmaceutical plants rely on these units for strict quality assurance tests. A well built humidity test chamber offers precise relative moisture regulation across extreme thermal ranges. Air circulation systems distribute moisture evenly to avoid condensation on sample surfaces. Advanced insulation prevents heat transfer to external lab work spaces.
Quiet refrigeration systems create a better working environment inside research labs. Modular panel designs allow custom sizing for specialized stability rooms. Precision steam generators deliver clean moisture without mineral scale buildup inside the cabinet. Color touchscreens simplify program setup for multi stage profile routines. Safety cutouts prevent overheating during continuous test runs.
Essential Features of Quality Environment Enclosures
Evaluation of climate enclosures requires checking sensor accuracy and control stability over long periods. Every top humidity chamber features air flow systems to eliminate temperature gradients. Interior illumination lets technicians inspect samples without disrupting internal equilibrium. Water purification accessories prevent mineral deposits on internal heating elements. Robust door locks prevent unauthorized access during critical stability studies.
Data logging capabilities satisfy strict regulatory compliance for electronic records. Backup power connections protect active test cycles against unexpected power failures. Compact cabinet designs maximize available floor space inside busy analytical laboratories. Clear view windows allow continuous visual checks on sample condition during long exposure tests.
Selection Criteria for High Precision Environmental Units
Buyers of a humidity test chamber must evaluate internal volume and airflow performance. Facilities must match cabinet size with weekly sample output requirements. Partnership with an experienced humidity test chamber manufacturer guarantees long term support and calibration services. Durable construction materials resist harsh chemical fumes and frequent cleaning cycles. Multi layer glass doors prevent condensation buildup during high moisture tests.
Service availability remains a vital factor when investing in environmental equipment. Local technical support minimizes delays when replacement parts or recalibration services are required. Uniform air distribution prevents localized hotspots that could alter test outcomes. User friendly interfaces reduce operator training time and prevent input errors.
Conclusion
Pharmaceutical research demands dependable climate simulation equipment for product safety. Presto Enviro leads with top local production while Thermotron Industries and Weiss Technik provide strong international solutions. Each manufacturer delivers unique features tailored to specific lab capacities and budgets. A high grade humidity test chamber safeguards product efficacy and protects consumer health across global supply chains. Quality testing infrastructure forms the backbone of safe pharmaceutical development.
Bub
Do?

Categories
Read More
Microsoft intensifies its battle against the persistent Conficker worm, offering a $250,000 global reward for information leading to the arrest and conviction of its creators. This unprecedented bounty highlights the company's profound frustration as infections surge despite a patch released months ago, compromising high-profile networks worldwide. Beyond the financial incentive, a major...
Daybreak Games recently surprised the EverQuest II community by announcing the revival of the retired Nagafen server as a free-for-all PvP seasonal beta. Borrowing heavily from the earlier Deathtoll server, this iteration features scoreboards, free trade, a one-character-per-account limit, and rebalanced stats. The plan was to launch the server for subscribers on February 5, but a last-minute...
Pierce Brosnan has been cast as Erick Erickssong, Lars' father and Iceland's most attractive man, in the upcoming musical comedy. The film stars Will Ferrell and Rachel McAdams as Lars Erickssong and Sigrit Ericksdottir, two hopeful Icelandic musicians. David Dobkin, known for directing Wedding Crashers and The Judge, helms the project. The screenplay comes from Will Ferrell and Andrew Steele,...
Fusion-Compiler für Anomalien Der Fusion-Compiler ist eine S‑Rang W‑Engine, konzipiert für Agenten mit Schwerpunkt auf Anomalien. Er erhöht sowohl den Grundangriffswert als auch das Penetrationsverhältnis und verstärkt zusätzlich die Anomalieeffekte von Spezial- und Ex‑Spezialangriffen. Als charakteristische Ausrüstung von Grace Howard hebt dieses Modul...
Sources within the Genshin Impact community indicate that Hoyoverse is preparing to introduce three new characters in version 6.3, marking an exciting addition to the game's evolving roster. This move seems to mirror the strategy seen in version 5.3 back in 2025, where the developers aimed for a strong start to the year by unveiling multiple new figures. Among the upcoming characters,...